AS9100D-aligned tooling and precision components for aerospace programmes.
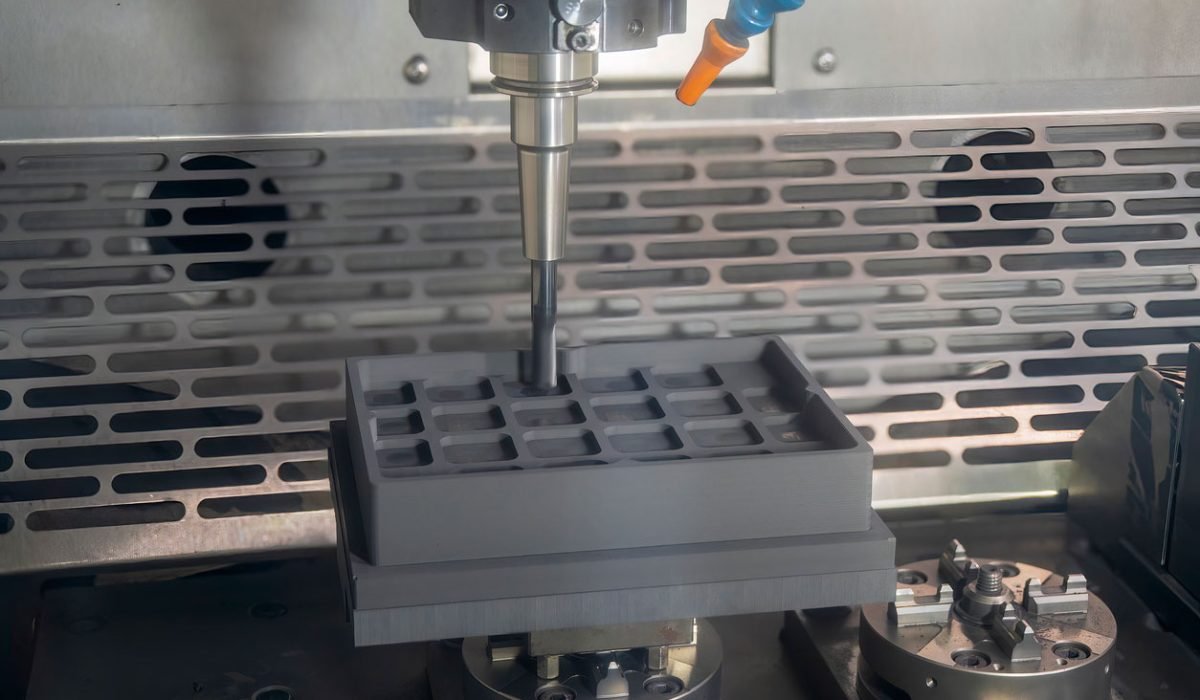
Aerospace work leaves no room for "close enough." Our aerospace capability covers full press-tool and die-set assemblies — top plates, stripper plates, die blocks, punch blocks, punch holders and die housings — machined and aligned to hold true through thousands of production cycles.
Our AS9100D certification scope specifically covers the manufacture of magnesium, aluminium, stainless steel and other ferrous and non-ferrous alloy products, including casting, precision work and machining for aerospace, defence and automotive applications.
Every component is backed by material verification against the mill certificate, in-process inspection and 100% final dimensional checks before release — the same documentation discipline aerospace customers audit for directly.
What We SupportPrecision-machined components and tooling supporting engine accessory mounts, housings and rotating/stationary hardware.
Tooling, fixtures and precision parts for actuation, interior fit-out and control-system component families.
Tight-tolerance shafts, housings and gear-train components manufactured for aircraft transmission assemblies.
Structural and mechanical components machined to the load-bearing tolerance landing-gear assemblies demand.
Beyond the plate stack, we manufacture the core tooling components that hold, guide and protect every punch and die — machined for flatness, parallelism and long service life.
This is the component that actually shapes or shears the part, so its wear resistance decides how many strikes the tool delivers before it needs regrinding. We select and heat-treat the alloy to the cutting or forming duty specified — harder for high-volume blanking, tougher where the tool sees shock-loading — and hold the cutting-edge geometry to the tolerance the customer's part drawing demands, since a few microns here shows up directly as burr or dimensional drift on every part the tool produces.
The core component that holds the die set together.
Provides a strong, accurate base for the die and other components.
Manufactured from high-grade alloy steel for strength and wear resistance.
Precision machined for flatness, parallelism and dimensional accuracy.
The punch block is what keeps a bank of punches moving on the same line, stroke after stroke, instead of drifting sideways and clipping the die. We bore each punch pocket on the same CNC setup as its mating hole in the die block, so the two components are machined as a matched pair rather than independently toleranced parts that happen to fit — which is what keeps clearance consistent all the way round a complex punch profile.
Holds and supports the punches in the correct position.
Ensures accurate movement and alignment during the stamping operation.
Designed for high load-bearing capacity and long service life.
The punch holder is the plate a toolroom actually opens up during maintenance, so we design it around fast, repeatable punch changeover as much as strength. Retaining faces are precision ground flat and square so a replacement punch seats correctly on the first try, and we offer keyed, shouldered or press-fit retention depending on how often the customer expects to swap punches on that particular tool.
Secures the punches and allows easy replacement.
Ensures precise guidance and alignment of punches during operation.
Heat treated and precision ground for durability and accuracy.
Available in various sizes and configurations as per requirement.
The die housing is the structural shell that keeps every internal component — die block, punch guides, ejectors — captured in correct relative position while protecting them from the surrounding press environment. We machine the internal pockets and the external mounting face in the same setup wherever the geometry allows, so the housing locates squarely on the press bed without needing shims, and we size wall sections to resist deflection under the full rated tonnage of the press it's built for.
Encloses and protects the die components.
Provides a rigid structure for mounting and alignment.
Ensures proper fitment of the die set in the press for accurate operation.
Precision machined for high strength, durability and dimensional stability.
This tooling work is also where our general product catalogue lives — shafts, housings, flanges and brackets built to the same precision standard.
Our ProcessWe review your drawing for tolerances, datums and material callouts, and flag anything that adds cost or risk before we quote.
Parts move through CNC milling, turning or heavy fabrication — matched to the job, run to the process plan we set at review.
Where a part calls for it, we heat-treat, grind, weld or surface-finish it to final spec, in-house.
100% dimensional inspection against the drawing, with full documentation, before a part ships.
ISO 9001:2015 & AS9100D-aligned inspection at every stage, not just the last one.
Material, machine, operator and inspection result recorded against every batch.
Prototype to production volume, planned and machined to the schedule you're quoted.
Machining, fabrication, finishing and inspection all happen in-house — no handoffs, no lost accountability.
CNC-machined tooling components, fixtures and precision parts for automotive manufacturing and tooling programmes, within our AS9100D scope for automotive applications.
View Details
CNC-machined precision parts and heavy fabricated assemblies for power-generation and energy-sector customers, including work for Bharat Heavy Electricals Limited (BHEL) and the Nuclear Power Corporation of India (NPCIL).
View Details
CNC-machined enclosures, chassis, housings and test fixtures for electronics and electronics-manufacturing-services (EMS) customers, held to tight dimensional tolerance for reliable assembly fit.
View DetailsSend us your specification and we'll respond with a process plan built to AS9100D scope.